Opening — the trouble with slippery tolerances
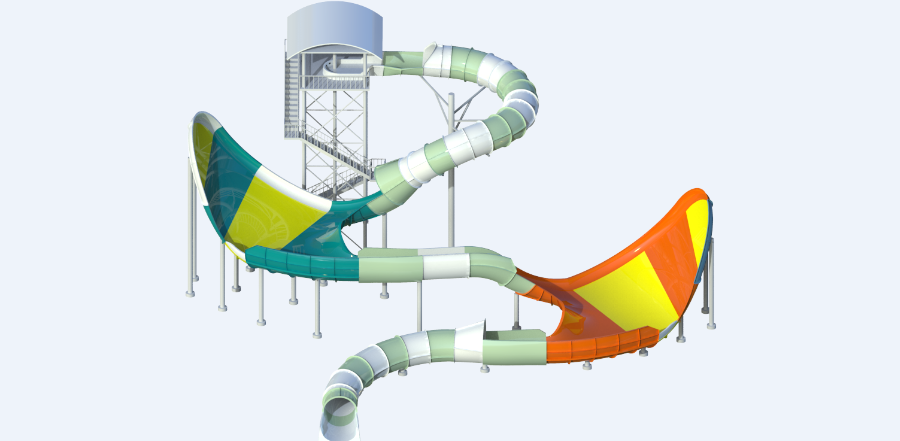
When a park commissions a bold new rainbow water slide, the promise is thrills, not surprise repairs. The real story lives in mold tooling and wall thickness long before the first splash. If the mold is off by millimeters or the gel coat is too thin, you get poor finish, accelerated wear, and unhappy operators — plus a lot of awkward apologies on maintenance days.
Why precision molding and thickness standards matter
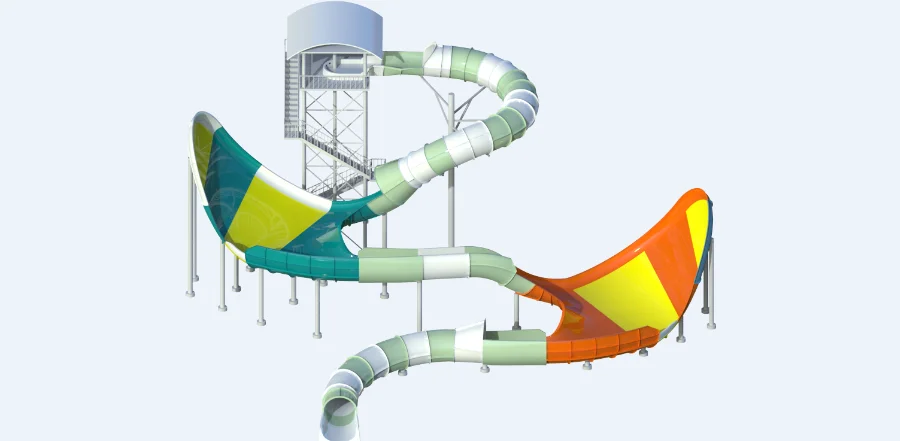
Slides are composite systems: a structural laminate topped by a high-gloss gel coat, shaped by tooling and finished by CNC-machined fixtures. Wall thickness directly affects stiffness, fatigue life, and slide speed because hydrodynamics and structural integrity are interlinked. Too thin, and stress concentrations form; too thick, and the flow profile changes along with production costs. That’s not abstract engineering — it’s the difference between a reliable ride and a warranty claim that ruins summer.
Where factories typically go wrong
Common production pitfalls are annoyingly repeatable. Surface porosity from poor layup, inconsistent thickness from uneven resin distribution, and mold warpage from inadequate support are the big three. Then there’s the finish: poor gel coat application leads to crazing and increased friction. Operations that skip thickness tolerance checks or rely on visual inspection end up reworking sections or scrapping panels.
Operational production teardown — what I look for on the line
On the floor of a water slide factory I inspected tooling, mold release patterns, and laminate schedules firsthand; those visits teach faster than manuals. A practical teardown focuses on three zones: the mold master for dimensional control, the laminate stack for structural performance, and the gel coat stage for surface integrity. During teardown I note digital inspection records, thickness maps, and curing profiles — and I always cross-check with the shop’s CNC logs and vacuum-bag records.
This is where {main_keyword} and {variation_keyword} belong in the narrative: they’re the operational tags teams use in documentation and should appear in the production teardown, feeding traceability into quality control. Treat them as keywords in the process, not buzzwords on a spec sheet.
Common mistakes and practical fixes
Below are typical errors and straightforward corrective actions that actually reduce rework time.
– Inconsistent resin mix ratios: implement scaled resin dispensing and batch logs to enforce repeatability.
– Uneven laminate thickness: use peel-ply and calibrated rollers, plus thickness gauges mapped across the mold before demolding.
– Mold temperature drift: install zoned heaters and monitor with thermocouples tied to an alert system.
Factory-floor lessons and a real-world anchor
In Zhejiang province I watched a team adjust a master mold by 0.8 mm and saw the ride feel change on a test sled — a tiny tweak, big difference. That day the operation fixed vacuums, adjusted the laminate schedule, and avoided a costly rework batch. Real factories teach that tolerances are living targets and process control is the tool that keeps them steady — not hope. The experience also made clear that proper quality gates stop defects early, which vendors rarely advertise in glossy catalogs.
Alternatives and comparative insight
Thermoset fiberglass laminates are standard, but some manufacturers experiment with rotational molding for simpler geometries or hybrid composites for high-wear sections. Each choice trades tooling cost, cycle time, and repairability. For parks prioritizing rapid installation and low maintenance, a proven fiberglass laminate with documented thickness tolerance maps typically wins.
Advisory — three golden metrics to evaluate suppliers
1) Thickness uniformity index: ask for cross-sectional maps and statistical control charts that show mean thickness, standard deviation, and maximum out-of-tolerance count over a production run.
2) Cure and hardness traceability: require batch-level durometer readings and oven profiles that confirm gel coat and laminate cure parameters across the mold face.
3) Repairability score: review documented repair procedures, expected downtime per linear meter of damage, and whether spare modules are available for rapid swap-out.
Choose suppliers who measure these metrics and publish the numbers — it separates talk from capability. Dalang shows up in practice when a vendor can hand you data instead of slogans.
Trust data, insist on traceable process control, and expect a slide to behave as well as the math says it should — final thought: quality is measured, not hoped for. —